


製造に関する洞察 — ペイオフ システム
ペイオフラックは複数のスプールを同時に処理できますか? それはライン速度にどのように影響しますか?
直接的な答えと、その背後にあるエンジニアリングのニュアンス - 張力、スピンドル数、同期が下流のすべてを静かに形作る方法。
直接の答え: はい、ペイオフ ラックは複数のスプールを処理できます。
A ペイオフラック can absolutely handle multiple spools simultaneously, and this is one of the most common configurations used in wire, cable, and hose manufacturing today.マルチスプールのペイオフ ラック。 ダブルスピンドルまたは多段ペイオフスタンド , allow two or more reels to unwind at the same time, feeding several strands into a single downstream process such as bunching, twisting, braiding, or extrusion. However, running multiple spools does affect line speed, tension consistency, and overall throughput in ways that operators need to understand before configuring their production setup.
ペイオフラック
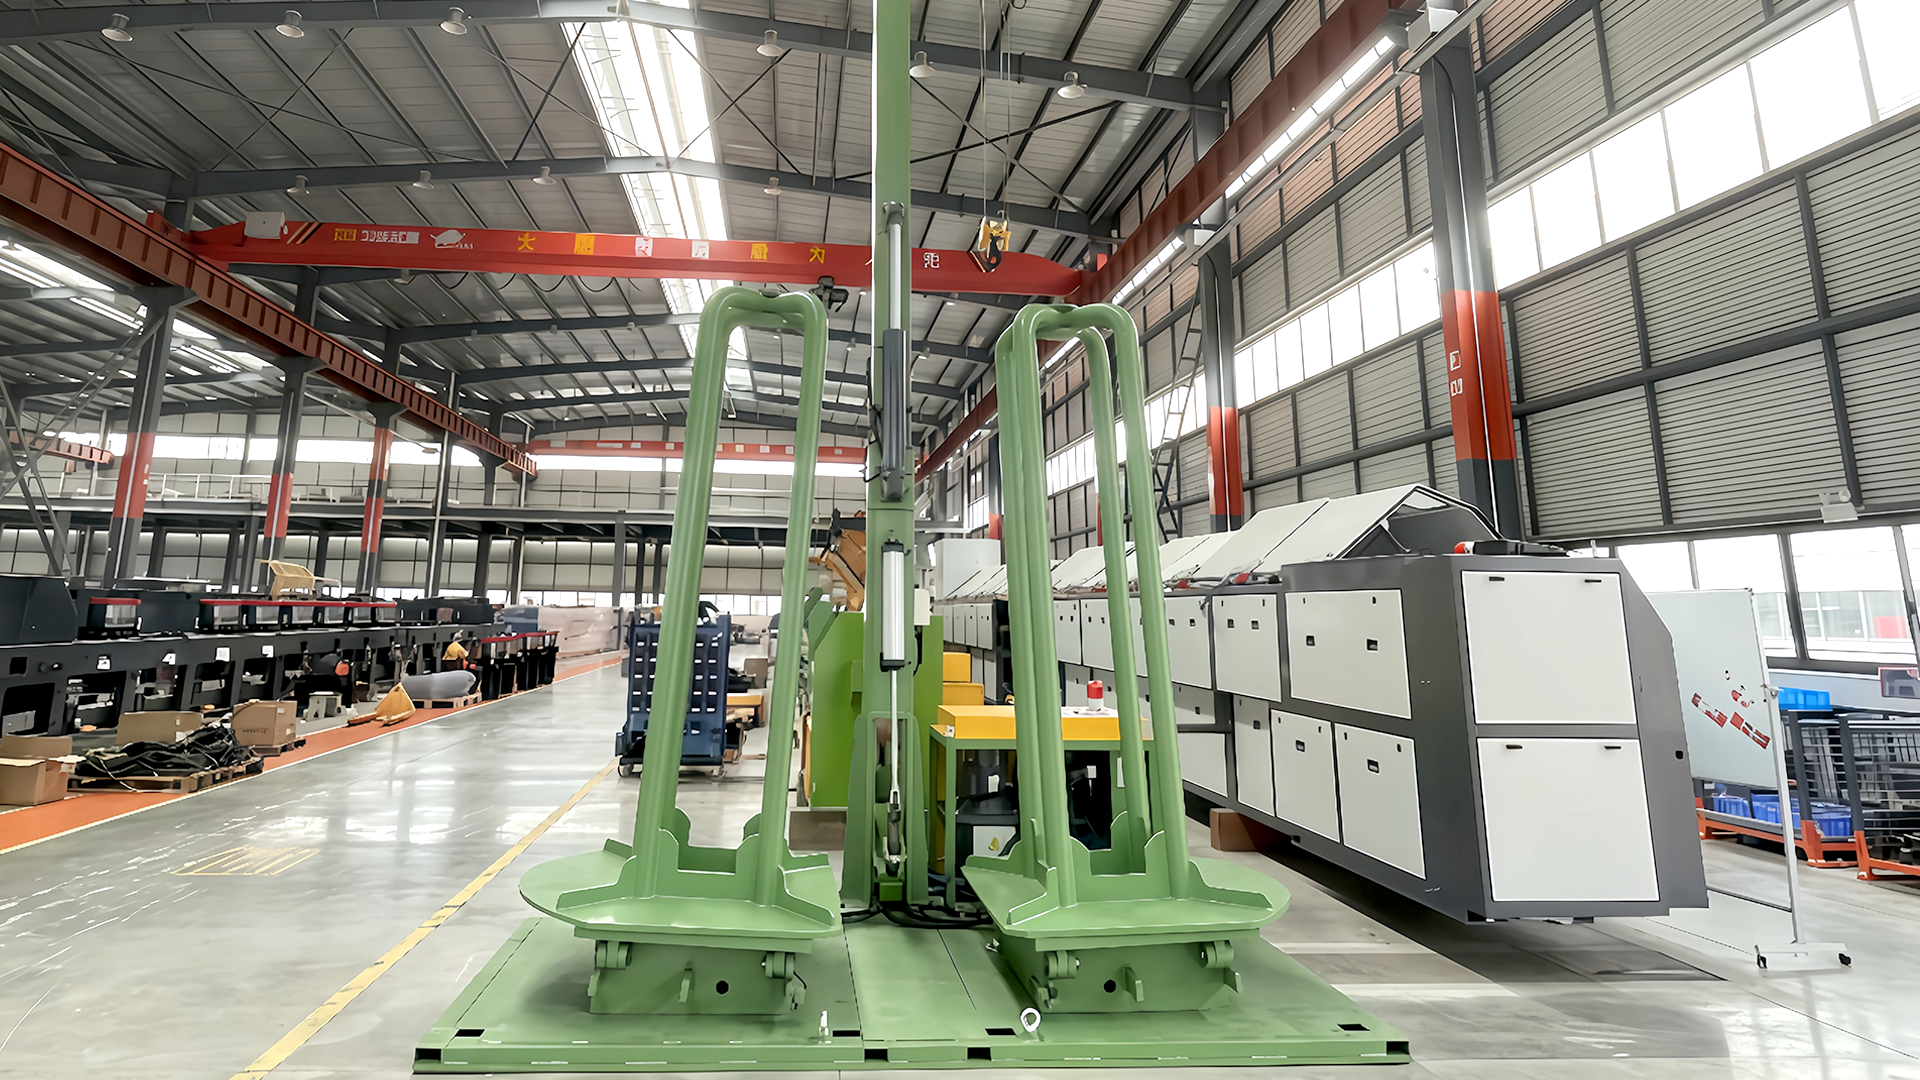
In general, adding more spools to a single pay-off rack increases the total mechanical load, the complexity of tension synchronization, and the risk of speed mismatches between spindles. When properly engineered, a multi-spool pay-off rack can maintain ライン速度はシングルスプール設定の 5 ~ 10% 以内 , but poorly matched components or inadequate braking systems can cause speed reductions of 20% or more due to constant stopping for tangle correction or tension adjustment.
メーカーがマルチスプールペイオフラックを使用する理由
Multi-spool configurations exist because many finished products require more than one strand of material fed into the process at once.たとえば、ツイスト ペア ケーブルでは、2 本の導体を完全に同期してほどく必要があります。 A braided hose reinforcement layer might need six, eight, or even sixteen spools of wire or fiber feeding simultaneously into a braiding head. Without a properly designed pay-off rack, this kind of multi-strand production simply would not be possible on a continuous basis.
一般的なアプリケーション
- ツイストペアおよび多心ケーブルの製造
- Wire braiding for shielded cables and reinforced hoses
- 複数の繊維ストランドを使用したロープとコードの製造
- Bundling operations for automotive wiring harnesses
- Fiber optic cable assembly requiring multiple buffer tubes
In each of these cases, a single pay-off rack replaces what would otherwise require several standalone unwinding units, saving floor space and reducing the number of operators needed to monitor the line.
"The bottleneck is rarely the machine — it's the one spool that doesn't match the others."
マルチスプールペイオフラック構成の種類
Not all multi-spool systems are built the same way. The configuration chosen depends heavily on the number of strands required, the diameter and weight of each spool, and the speed at which the downstream machine operates.
サイド・バイ・サイドのスピンドルラック
This is the simplest form of multi-spool pay-off rack, where two or more spindles are mounted horizontally next to each other. Each spindle rotates independently with its own braking mechanism, and the strands are guided through separate tensioners before merging at a common feed point. This design works well for low to moderate speed applications, typically under 150 meters per minute.
垂直多段ペイオフスタンド
より多くのスプールを必要とする操作の場合は、垂直多層 支払いスタンド スピンドルを塔状に積み重ねます。 This saves significant floor space compared to a side-by-side layout and is commonly used in braiding machines where eight, sixteen, or even twenty-four spools need to feed into a single braiding head simultaneously.
回転ドラムまたはクリールスタイルのラック
Creel systems house dozens of spools in a fixed frame, with each spool feeding a separate strand outward. These are typically used in textile-adjacent wire operations or in cable armoring processes where a large number of thin wires must be fed in parallel with minimal tension variation.
複数のスプールがライン速度に与える影響
スプール数とライン速度の関係は線形ではありませんが、重要です。 Each additional spool introduces another potential point of failure, another tension curve to manage, and another source of mechanical inertia that must be overcome during acceleration and deceleration.
スプールの直径、重量、または制動抵抗が一致しない場合、「最も遅い」スプールからのストランドがライン全体のボトルネックになります。オペレータは多くの場合、次のような理由で全体の回線速度を低下させます。 10%~25% simply to accommodate the least consistent spool in a multi-spool setup, even if the other spools could technically run faster.
| スプール数 | 一般的なライン速度への影響 | 共通アプリケーション |
|---|---|---|
| 1スプール | ベースライン (100%) | 単線伸線 |
| 2スプール | ベースラインの 90 ~ 95% | ツイストペアケーブル |
| 4~8スプール | ベースラインの 75 ~ 90% | 小さな編み込み作業 |
| 16 スプール | ベースラインの 60 ~ 80% | 重厚な編組シールド、装甲 |
これらの数値は業界の一般的な推定値であり、張力システムの品質、巻き戻される素材、およびスピンドルの位置合わせの精度によって異なります。 Facilities that invest in matched-tension spindles and automated braking often see far smaller speed penalties, sometimes keeping losses under 5% even with eight or more spools running at once.
複数のスプール間の張力の同期
張力制御は、マルチスプールペイオフラックを確実に機能させる上で最も重要な要素です。 If one spool feeds material too loosely while another feeds too tightly, the resulting product can suffer from inconsistent diameter, uneven twist geometry, or outright breakage.
機械式ブレーキシステム
Simple friction brakes or magnetic particle brakes are applied to each spindle individually. These are cost-effective and work well for lower-speed lines, but they require regular manual calibration to keep tension consistent across all spools.
ダンサーアームシステム
ダンサー アームは、リアルタイムの張力測定値に基づいてブレーキ圧力を自動的に調整する、バネ式または空気圧式のアームです。 In multi-spool setups, each strand typically gets its own dancer arm, allowing the pay-off rack to self-correct minor tension fluctuations without operator intervention.
サーボ駆動のアクティブペイオフラック
高速または高精度のアプリケーションの場合、サーボ モーターは純粋に受動的なブレーキに依存するのではなく、各スピンドルをアクティブに駆動します。これは最も高価なオプションですが、すべてのスプールにわたって最も一貫した張力を提供し、多くの場合、マルチスプール ラインを以下の速度で実行できます。 シングルスプール同等品の 3 ~ 5% .
スプールを追加する前の実際的な考慮事項
追加のスプールに対応するためにペイオフ ラックをスケールアップする前に、コストのかかるダウンタイムや製品の欠陥を回避するために、いくつかの実際的な要素を評価する必要があります。
- スピンドルベアリングとフレームが、荷重がかかるすべてのスプールの合計重量をたわむことなく支えられることを確認します。
- Verify that each spool has matching or near-matching diameter and material type to reduce tension mismatch.
- ストランドの交差や摩耗を防ぐために、ガイドアイとテンショナーの間隔が正しいことを確認してください。
- 下流の機械の巻き取り速度が、新たなボトルネックになることなく追加のストランドを実際に使用できるかどうかを評価します。
- Plan for spool changeover time, since more spools mean more frequent individual replacements even if the overall run length increases.
この評価を省略した施設は、もつれ修正やスプール交換のための計画外の停止により、理論上のスループットの向上が相殺されるため、新たに拡張されたペイオフ ラックが実際には予想よりも低い純生産量を生成していることが判明することがよくあります。
マルチスプール システムのメンテナンスへの影響
スプールが増えると可動部品も多くなり、可動部品が増えるとそれに比例してメンテナンスの負担も大きくなります。シングルスプールペイオフスタンドでは、ベアリングの潤滑とブレーキパッドの検査を数か月ごとに行うだけで済みますが、マルチスプールラックを継続的に稼働させる場合は、テンショナー、ガイドローラー、スピンドルの位置合わせを毎週チェックする必要がある場合があります。
摩耗パターンはラック全体で異なることが多いため、マルチスプール ラックを管理するオペレータは、個々のスピンドル位置ごとにメンテナンス ログを保管する必要があります。たとえば、駆動機構の近くに配置されたスピンドルは、フレームの外縁にあるスピンドルよりも振動に関連した摩耗が多くなる可能性があります。
スループット向上と複雑さのバランスをとる
マルチスプール ペイオフ ラックの主なトレードオフは単純です。スプールが増えると、サイクルごとに処理されるストランドの数も増えますが、複雑さが増し、潜在的な障害点が増加し、通常は達成可能なライン速度が若干低下します。ほとんどのメーカーにとって、最終的な効果は依然としてプラスです。これは、4 つまたは 8 つの別個のシングルスプール ラインを最高速度で稼働させ、追加の労力と床面積を必要とする場合よりも、シングルスプール速度の 85% で 4 つまたは 8 つのストランドを供給する方が、1 時間当たりはるかに多くの最終製品を生産できるためです。
より多くのスプールを処理するためにペイオフ ラックを拡張する決定は、製造される特定の製品、その製品の張力変動の許容範囲、およびより高精度の張力調整装置に投資できる資本と常に比較検討する必要があります。適切に設計されたマルチスプールペイオフスタンドとアクティブ張力制御を組み合わせることで、生産効率の向上を実現できます。 30%以上 ストランドごとの速度が若干低下することを考慮したとしても、複数のシングルスプールラインを個別に実行する場合と比較して。
重要なポイント
- マルチスプールペイオフラックは、ツイスト、編組、束ねられたケーブル製品に標準装備されています。
- ライン速度は、スプール数と張力制御の品質に応じて、通常 5% ~ 25% 低下します。
- サーボ駆動のアクティブ システムは速度損失を最小限に抑えますが、初期費用が高くなります。
- すべてのポジションでスプールのサイズと素材を一致させることで、張力の不一致とダウンタイムを軽減します。
- 速度のトレードオフにもかかわらず、マルチスプール構成は通常、複数のシングルスプールラインを実行するよりも全体的な生産効率が高くなります。


